Our land is rich in natural gifts. Among them, a special place belongs to precious, semi-precious, and ornamental stones. It is no wonder that working ornamental stone attracts many craftsmen and enthusiastic amateurs. And to do this successfully, desire and talent alone are not enough — you need special tools and at least a minimum of equipment; diamond disc saws and fixtures for cutting ceramic tile. However, there are two “buts.” First, their field of application is quite limited (for example, diamond discs are 2 mm thick or more, which in many cases is unacceptable for cutting ornamental stones). Second, their cost is, to put it mildly, out of proportion to the modest means of an average working Russian, and even more so of a pensioner.
Therefore, when I became interested in crafts made from natural stone, taking the above into account, the first thing I decided to do was to design and make a small cutting machine. As a result, a stone-cutting circular saw (KCP) appeared — fairly simple to manufacture, convenient and effective in use.
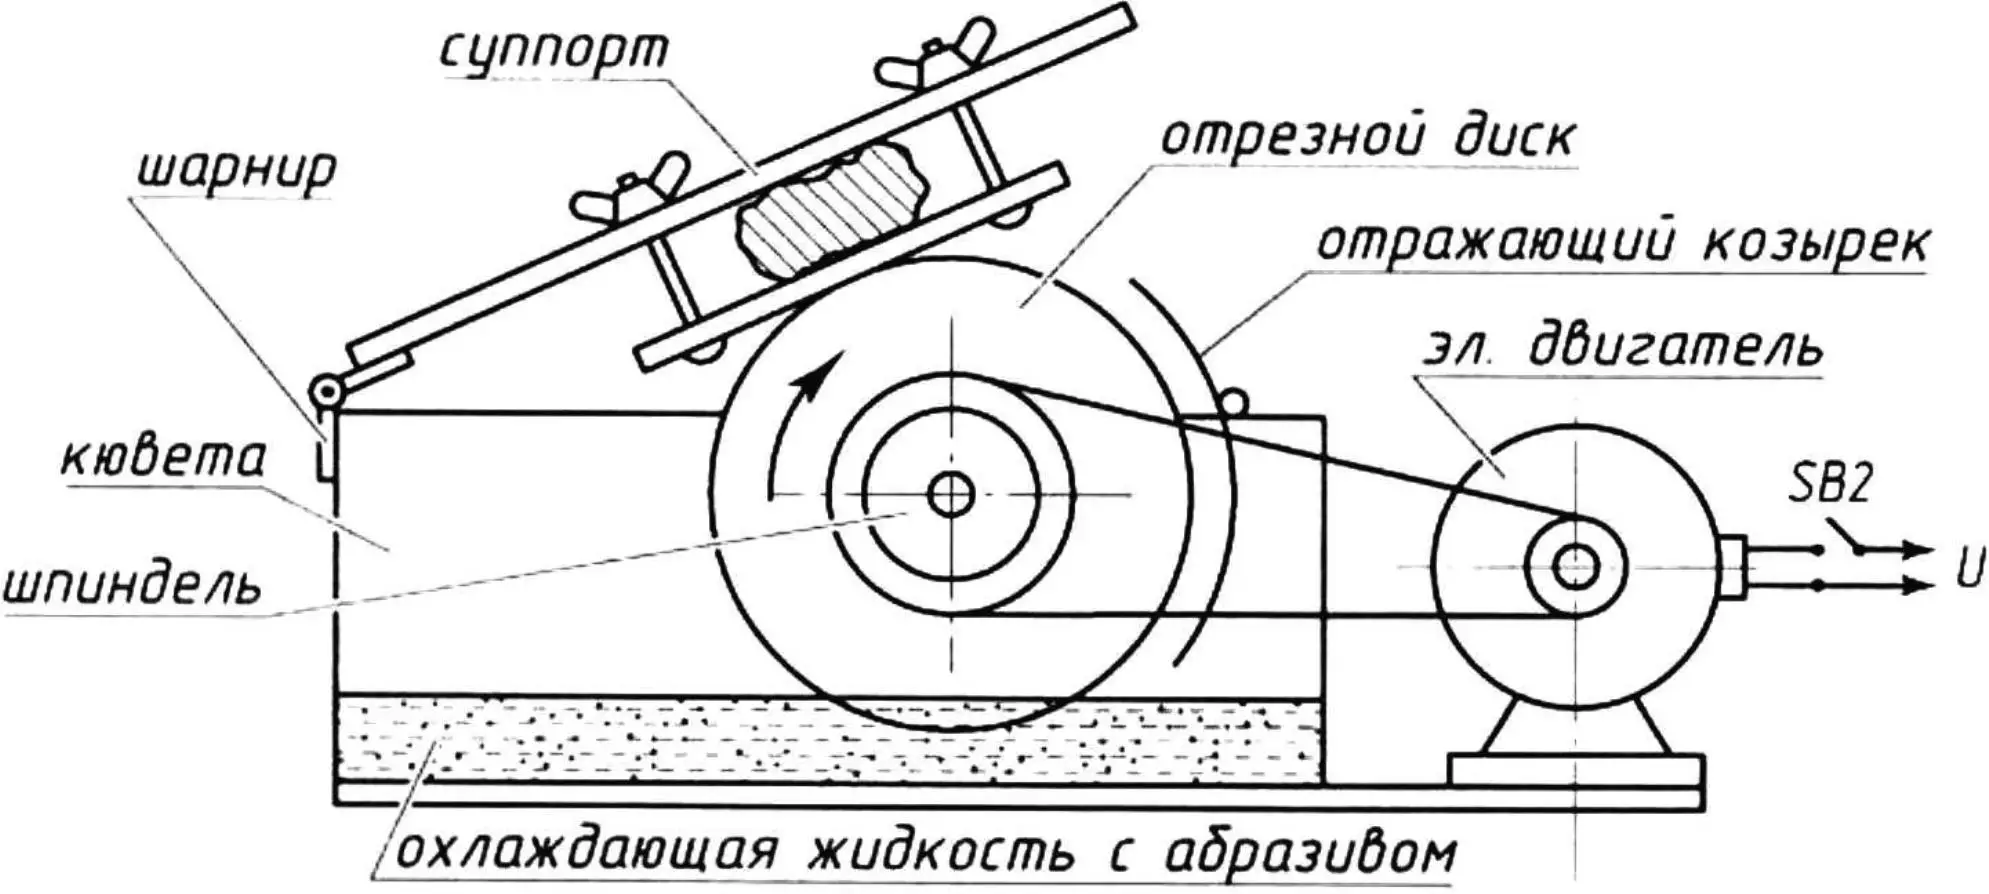
The operating principle of the KCP is very simple (Fig. 1). Abrasive powder, for example silicon carbide, is added to a tray with coolant. As the cutting disc rotates, it “picks up” the abrasive and, at the point of contact with the stone being cut — which is fixed on the KCP support — scratches a groove that deepens with each revolution until the stone is split in half. Using free abrasive as the working medium instead of, say, diamond wheels has some undeniable advantages. First of all, its cost is an order of magnitude lower, and this, as noted above, is of no small importance. In addition, it makes it possible to use cutting discs of practically any required size. And this, too, will not require large expenses, because the discs (they are made from roofing iron) can easily be made by yourself. But one drawback should also be kept in mind: the cutting rate with free abrasive is considerably lower than with a diamond wheel.
Structurally, the KCP consists of two main assemblies: the working unit (Fig. 3) and the power supply unit, placed at some distance from the former (this is done to improve electrical safety during operation). A 12 V DC electric motor from a car radiator cooling fan is used as the drive (Fig. 4). The motor housing was slightly modified: two of the three standard mounting elements were removed. The motor is placed in a clamp made of galvanized sheet metal and, by means of a loop at its end and an M6 stud, is pivotally mounted in angle brackets on the base. A drive pulley is screwed onto the motor shaft and secured with a 2 mm diameter pin. Rotation is transmitted to the working spindle by a V-belt (from the generator drive of a Zhiguli car). For belt tensioning, the motor housing is connected to a shackle through the remaining mounting element. Next to the motor, brass terminals for connecting it and control buttons in a special housing are mounted on the base. The buttons are from an old vacuum-tube TV (it is better to use an ordinary toggle switch of the TV-1-1 type).
The base housing (bottom, supports, front, side, and rear walls) is made of birch boards 20 mm thick (Fig. 5). The walls are joined with a tongue-and-groove joint and glued to the bottom. For reliability, the parts are additionally fastened with screws. After assembly, the housing was impregnated with heated drying oil and painted with oil paint.
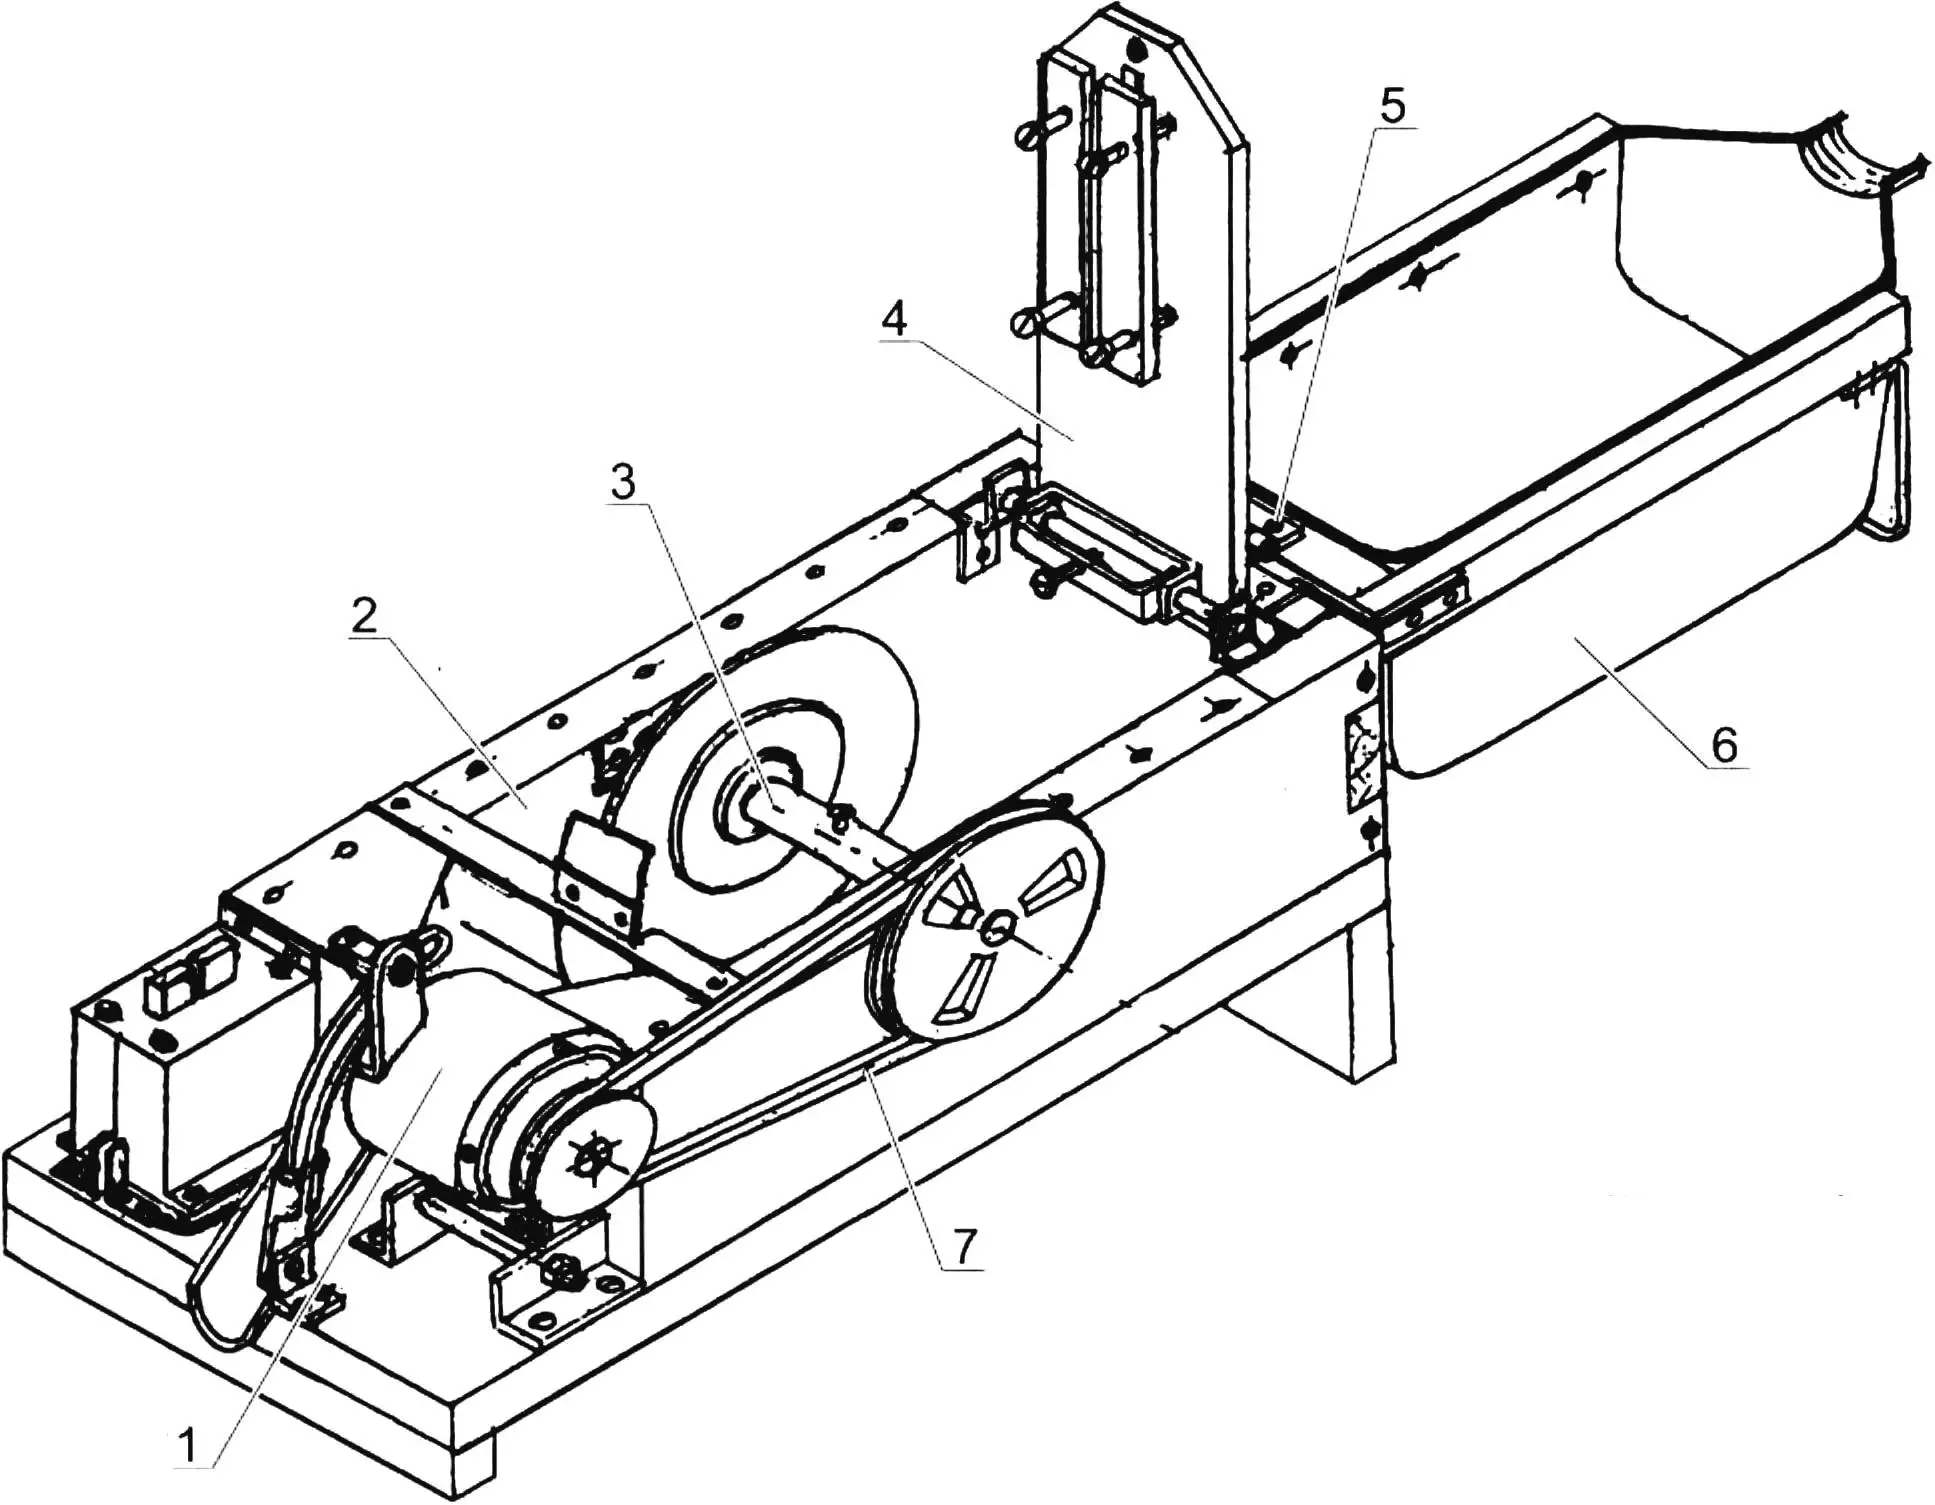
1 — motor (from a car radiator cooling fan); 2 — base; 3 — spindle; 4 — support; 5 — butt hinge; 6 — lid; 7 — belt (from a Zhiguli generator drive)
Next, a 5-liter plastic drinking-water bottle is inserted into the base; a recess for its neck is cut in the front wall to fit. Then the bottle is cut lengthwise at the height of the base walls. The resulting tray is nailed around its perimeter to the base walls with small nails. Under the tray neck, a trough made of galvanized sheet metal 0.8 mm thick is attached to the front wall, and lid retainers are installed on top. The upper ends of the side walls are covered with reflective strips 30 mm wide cut from plastic bottles. The strips are fastened with a lap toward the inside of the base using small nails. They protect the gaps and joints between the base walls and the tray from coolant with abrasive getting in during KCP operation. In addition to these parts, a shackle for fastening the motor when tensioning the belt, a central deflector, and support mounts are installed on the base.
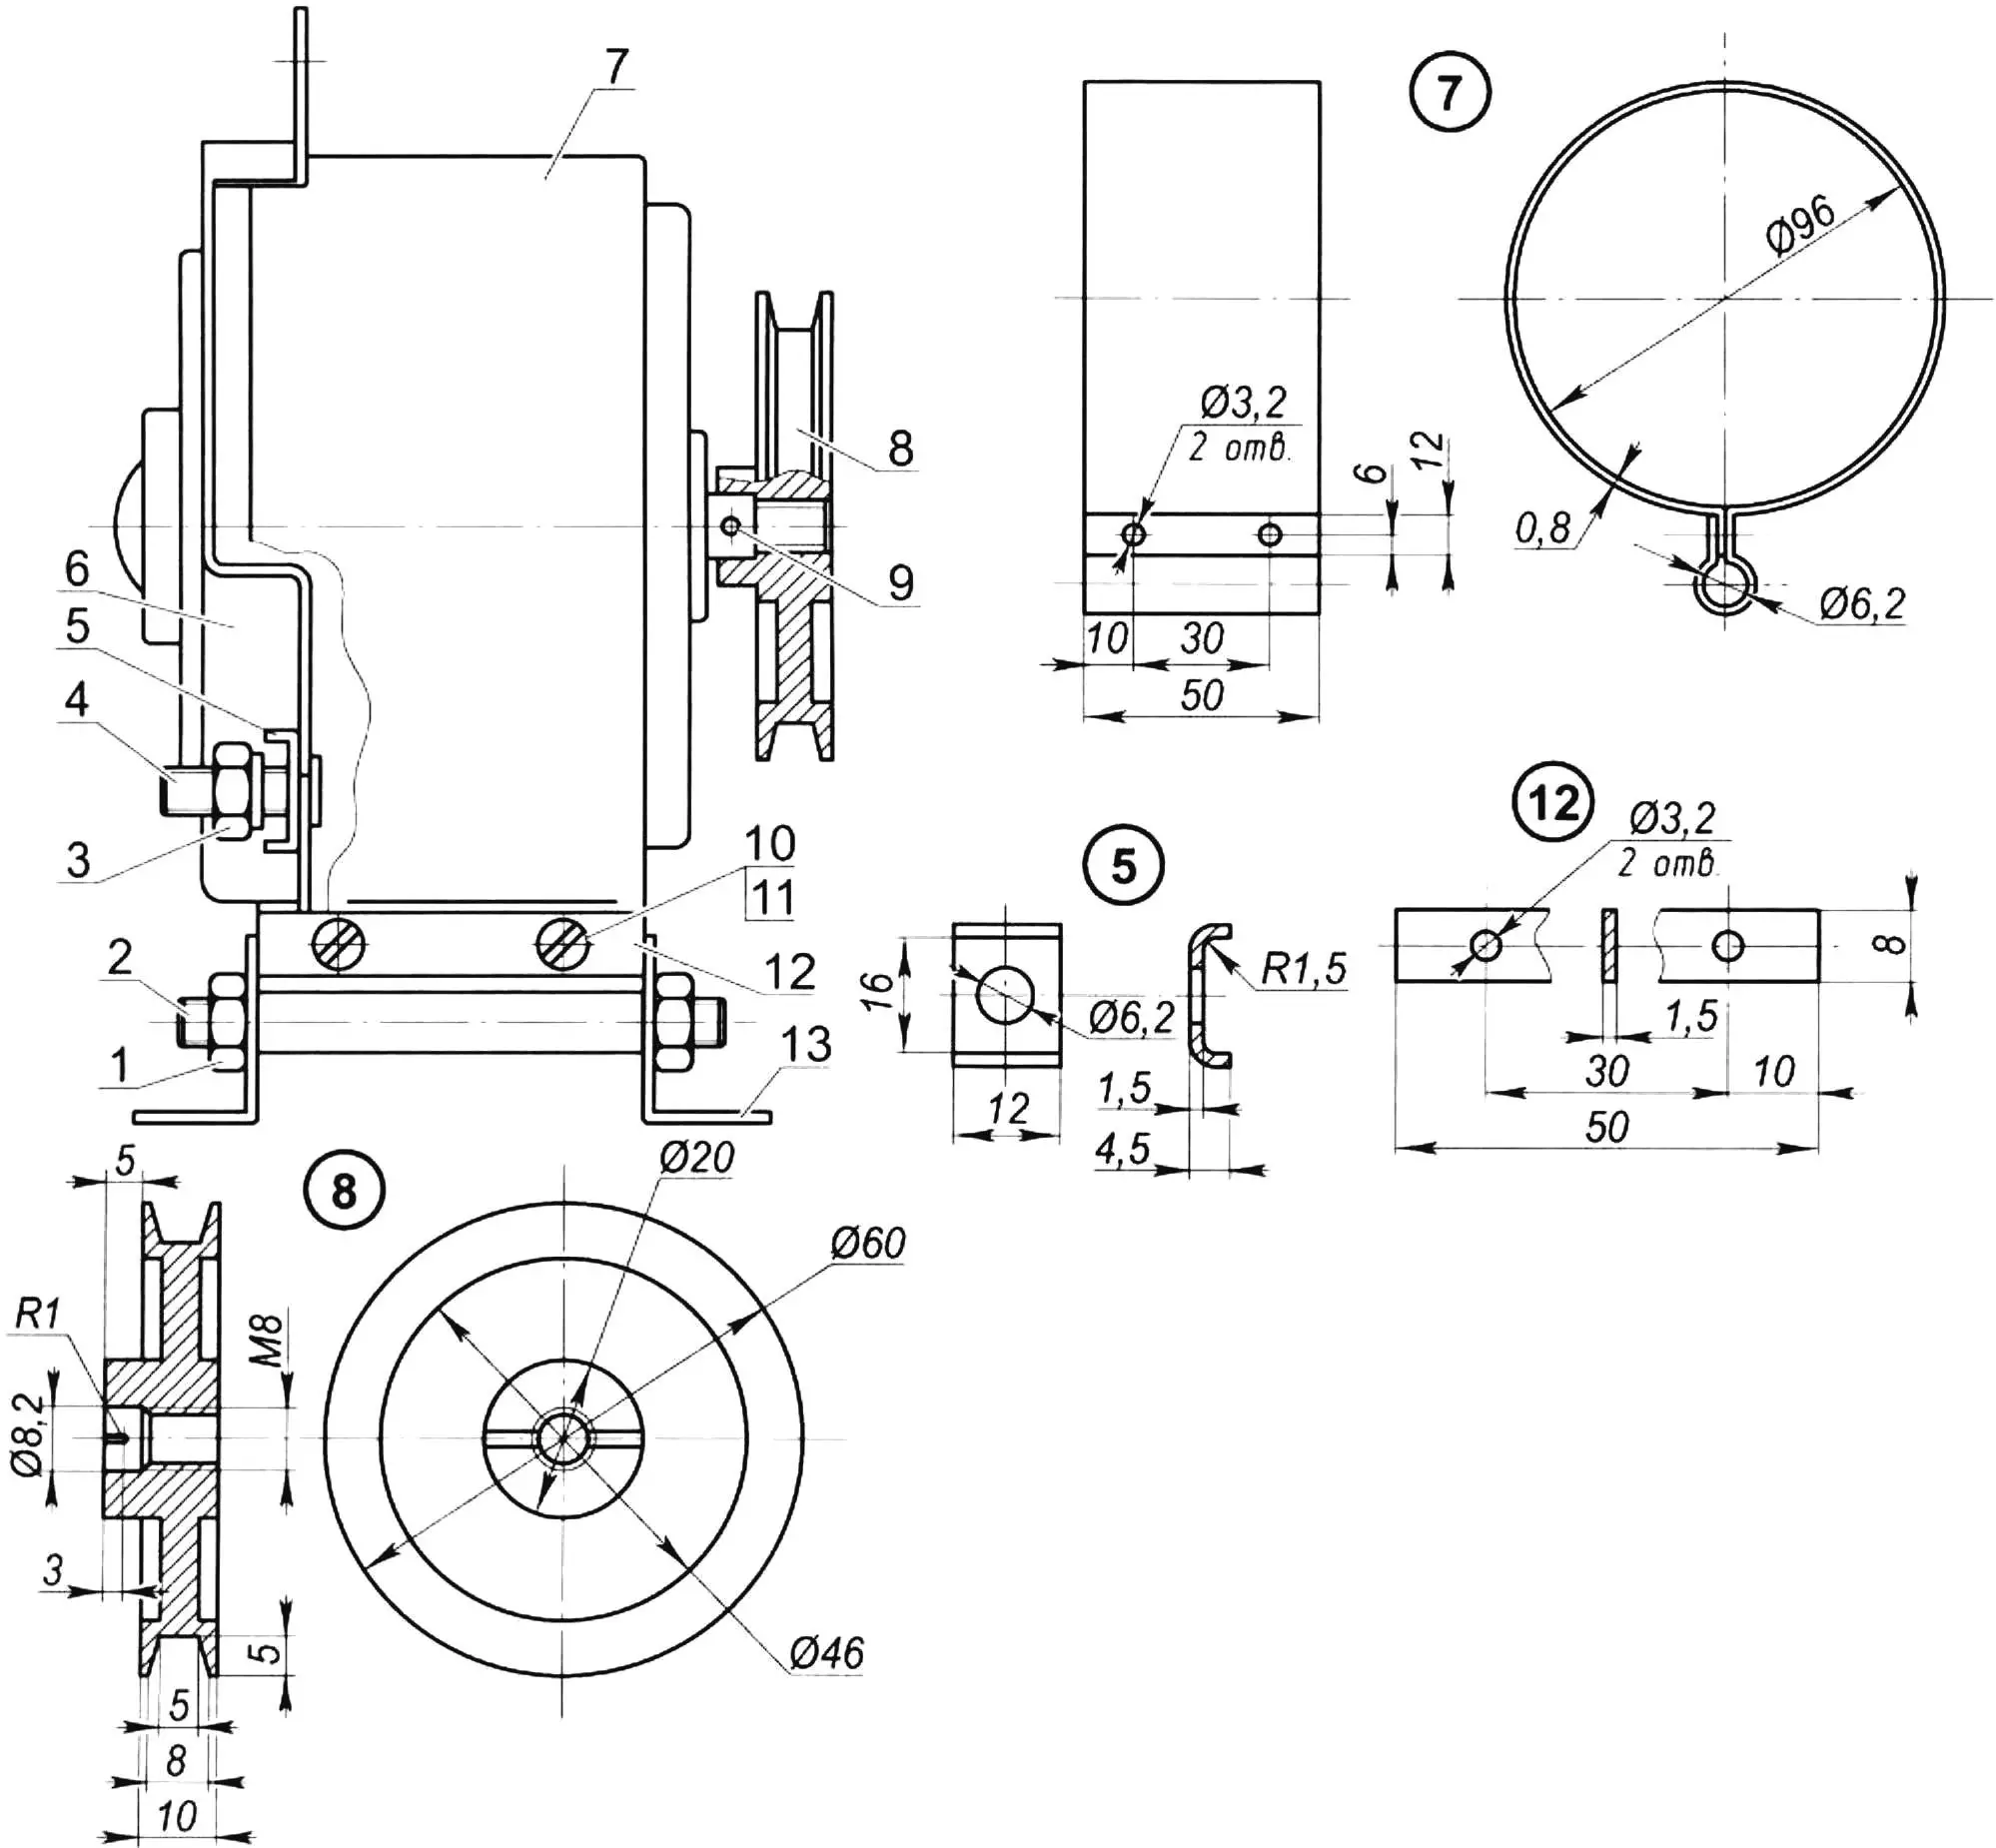
1 — M6 nut (2 pcs.); 2 — M6x65 stud; 3 — M6 terminal nut; 4 — terminal (M6 bolt); 5 — special washer; 6 — electric motor; 7 — clamp (galvanized sheet metal s0.8); 8 — pulley; 9 — pin (Ø2×14); 10, 11 — M3 bolt and nut (2 sets); 12 — strip (steel, bar 1.5×8, L50, 2 pcs.); 13 — motor mounting angle to the base (2 pcs.)
After that we proceed to assembling and installing the working spindle (Fig. 8). First of all, we determine the shaft position. To do this, we fasten the motor to the shackle as shown in Figure 3, put the belt on the drive and driven pulleys, and tension it by shifting the driven pulley toward the rear wall of the base. With the pulley fixed, through the hole in its hub we mark on the side wall of the base the center of the hole for the spindle shaft. We transfer the marking to the opposite wall and drill holes 11–12 mm in diameter in the side walls. Then we fasten the driven pulley on the end of the shaft, put one bearing plate on the shaft, pass it through the right wall of the base, put on two more, and pass it through the left wall. On the free end of the shaft we put the last, fourth plate and fasten them all in sequence, ensuring light tension of the drive belt and free rotation of the shaft. Next we remove the shaft from the base, fill the holes in the side walls with grease of the CIATIM-201 type and, returning the shaft to its place, successively put washers on it, a bushing with the cutting disc fastened to it, and a spring. Finally, the bushing is fixed on the shaft with a set screw.
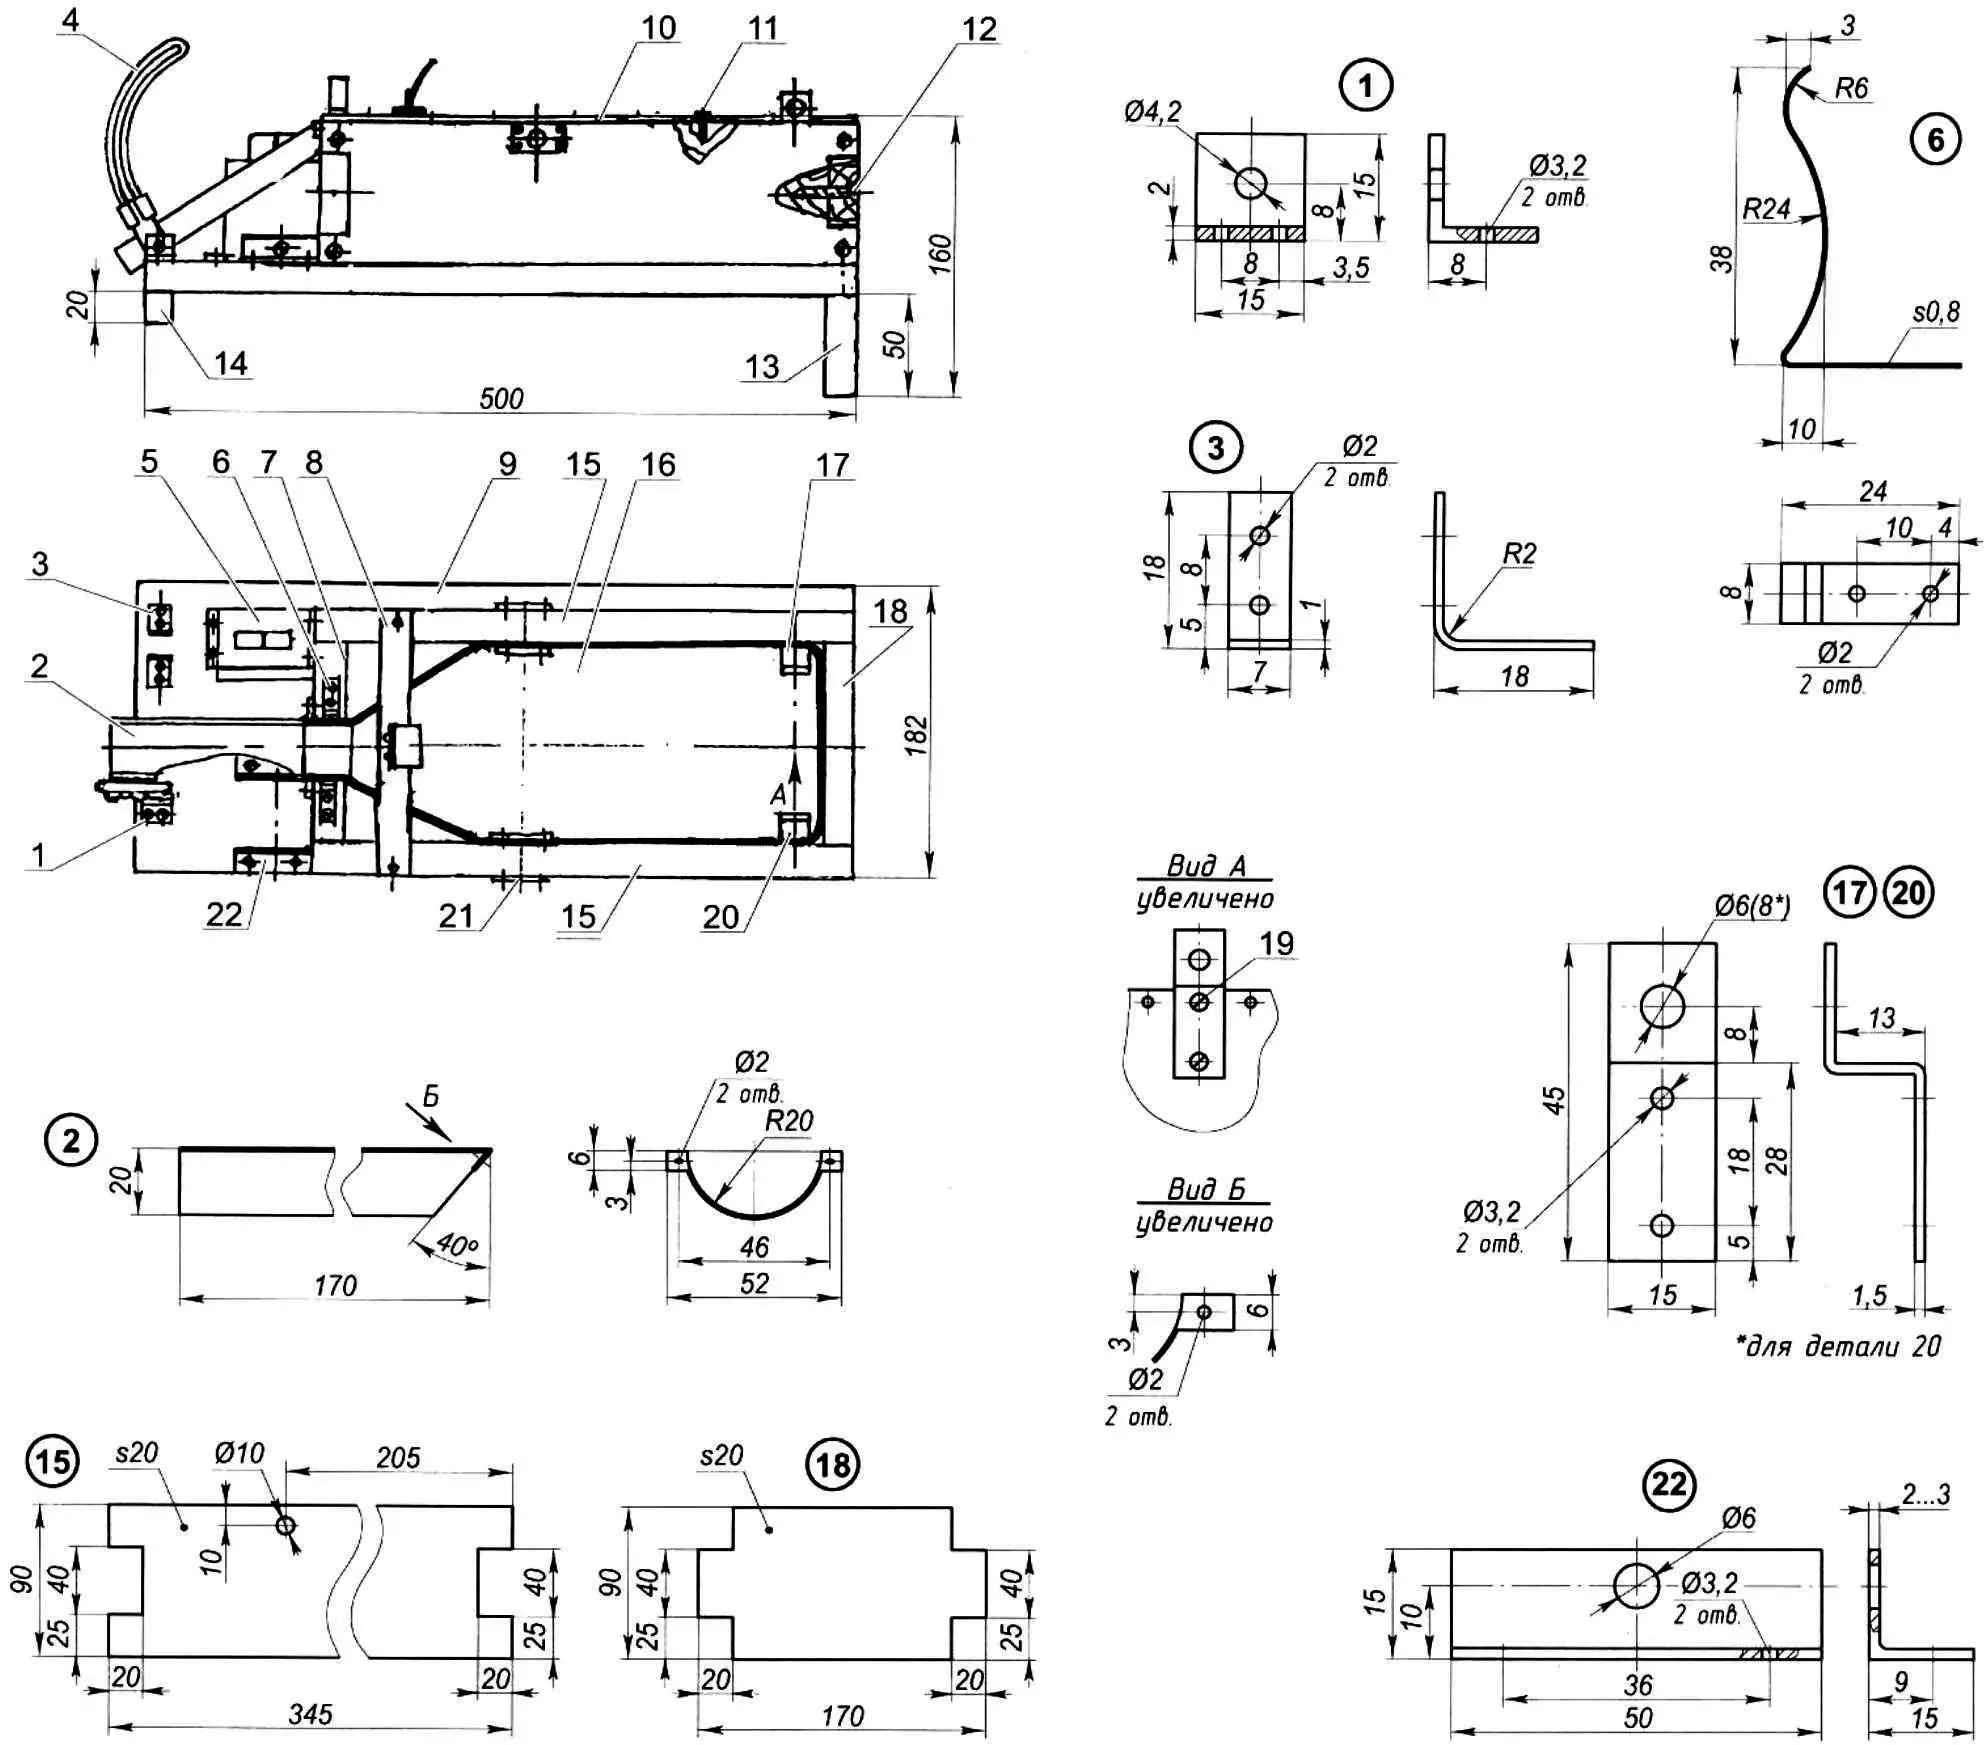
1 — shackle mounting angle (angle 15×15); 2 — trough (galvanized sheet metal s0.8); 3 — contact (brass, 2 pcs.); 4 — shackle; 5 — switch (from a vacuum-tube TV or a TV-1-1 type toggle); 6 — lid retainer (galvanized sheet metal s0.8); 7 — front wall; 8 — central deflector; 9 — bottom; 10 — reflective strip (cut from a plastic bottle, 2 pcs.): 11 — nail (Ø1×10, 30 pcs.); 12 — screw (Ø3.5×40, 12 pcs.); 13 — rear support; 14 — front support; 15 — side walls; 16 — tray (half of a plastic 5-liter bottle); 17, 20 — support mounts (steel, bar 1.5×15); 18 — rear wall; 19 — screw (03×20, 4 pcs.); 21 — bearing plate (4 pcs., installed during spindle mounting); 22 — motor mounting angle (duralumin, angle 15×15, 2 pcs.); material of parts 7,9,13,14,15,18 — birch board s20; on the top view, reflective strips 10 are conventionally not shown
The support (Figs. 3, 9) serves to hold the stone being cut and to feed it to the cutting disc. The stone is clamped between a plate and two bars made of sheet getinaks 6 mm thick. In the plate, between the bars, a slot is cut for the cutting disc to pass through, and a 2 mm hole is drilled near the end; it is used to fasten a thread and hang a weight when it is necessary to increase the workpiece pressure against the tool. The thread passes through the tray neck and then along the trough. Installing the support is not difficult and is clear from the drawings shown. The main task is to fix the plate with an M5 set screw so that the cutting disc is on the axis of the slot.
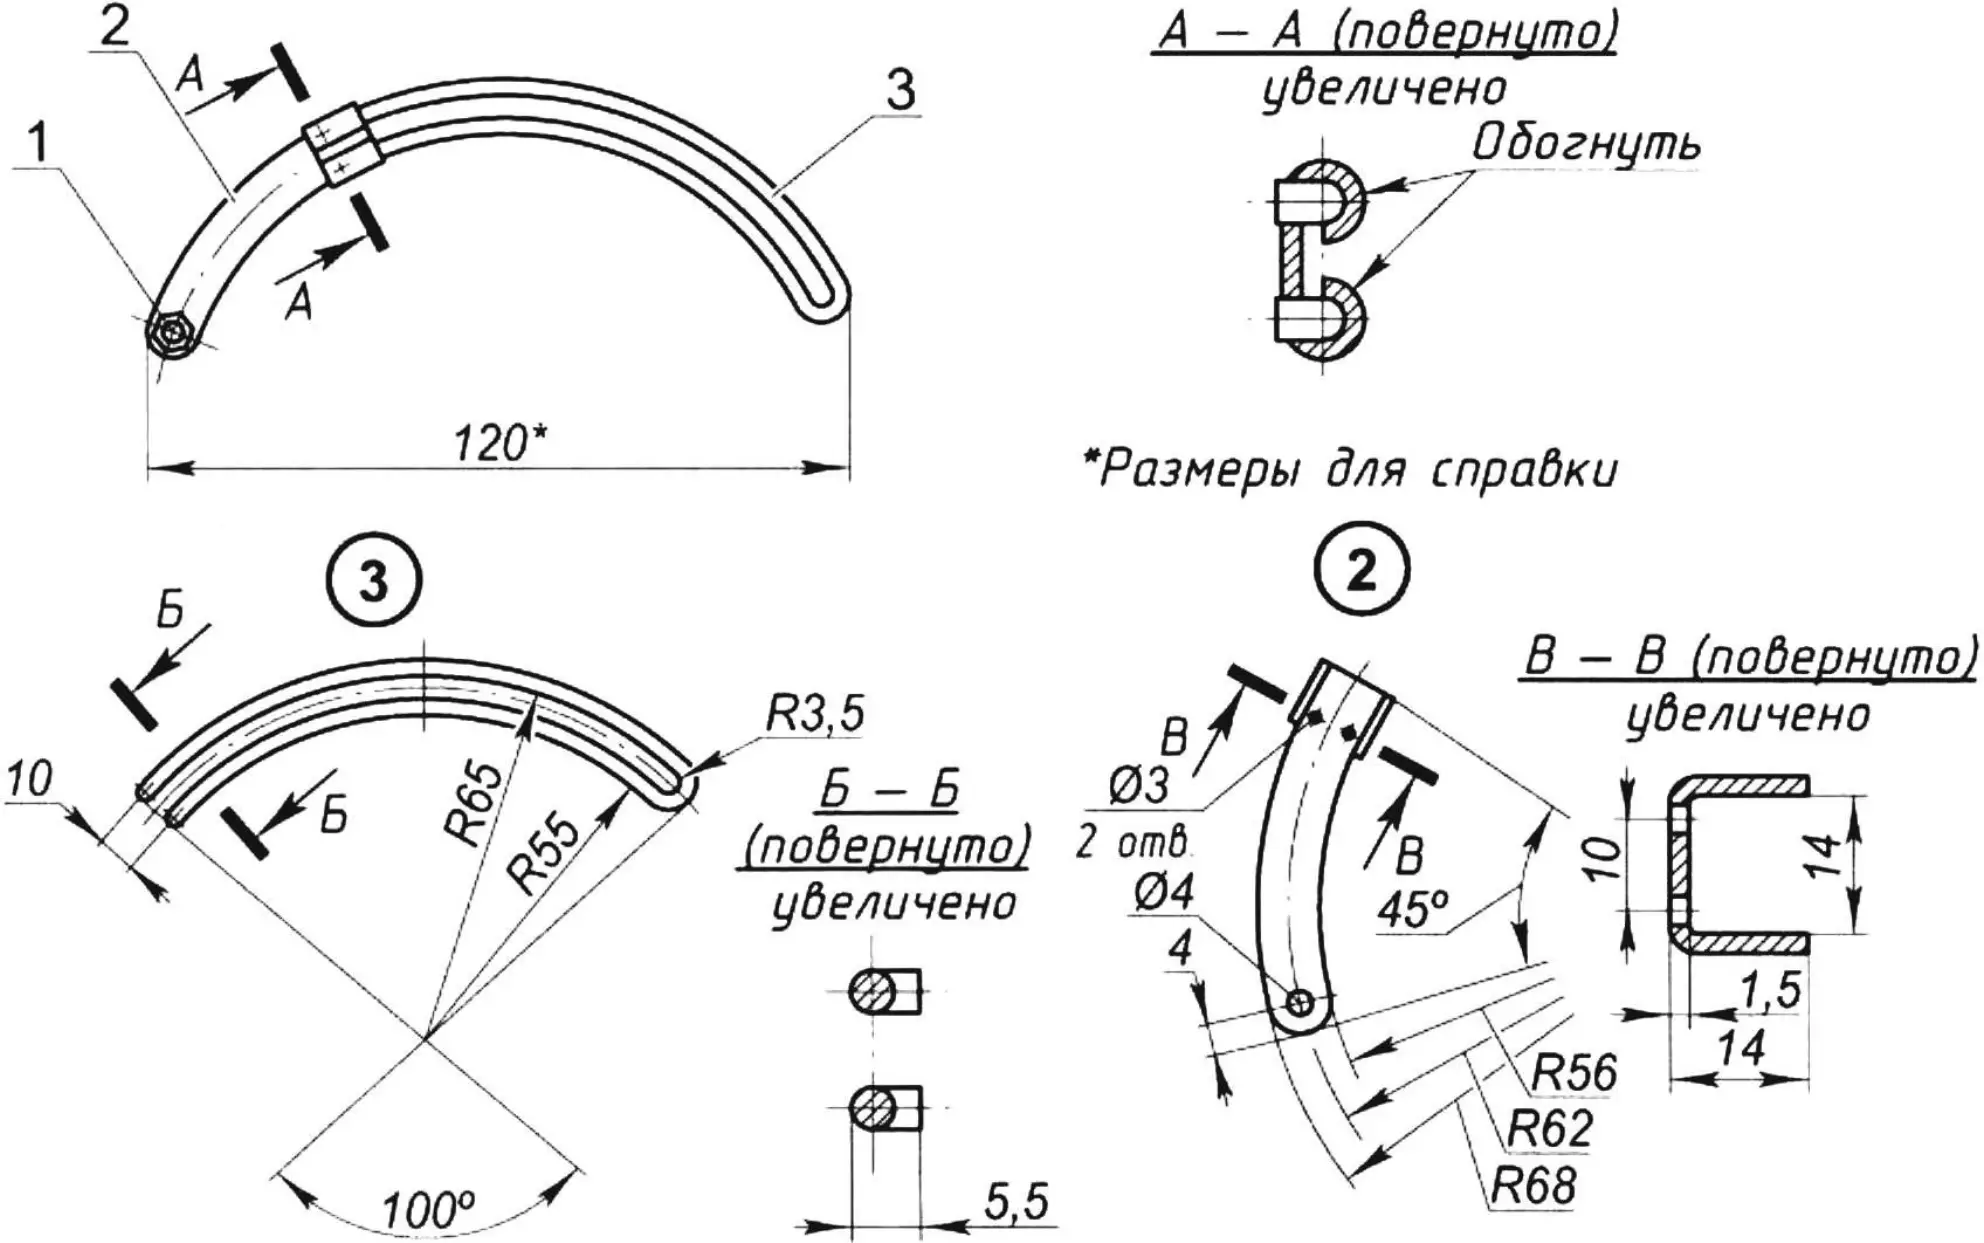
1 — axle (bolt, M4 nut, washer); 2 — holder (steel, sheet s1.5); 3 — arc (wire Ø3)
The lid (Fig. 10) consists of a wooden U-shaped frame assembled from birch bars, a closing clamp made of 3 mm wire, and a housing (half of a plastic 5-liter bottle — the remainder from the tray). The lid is attached to the base with a small butt hinge.
Work on the KCP is done as follows. First, coolant is poured into the base tray — a mixture of water and motor oil in a ratio of about 15:1.
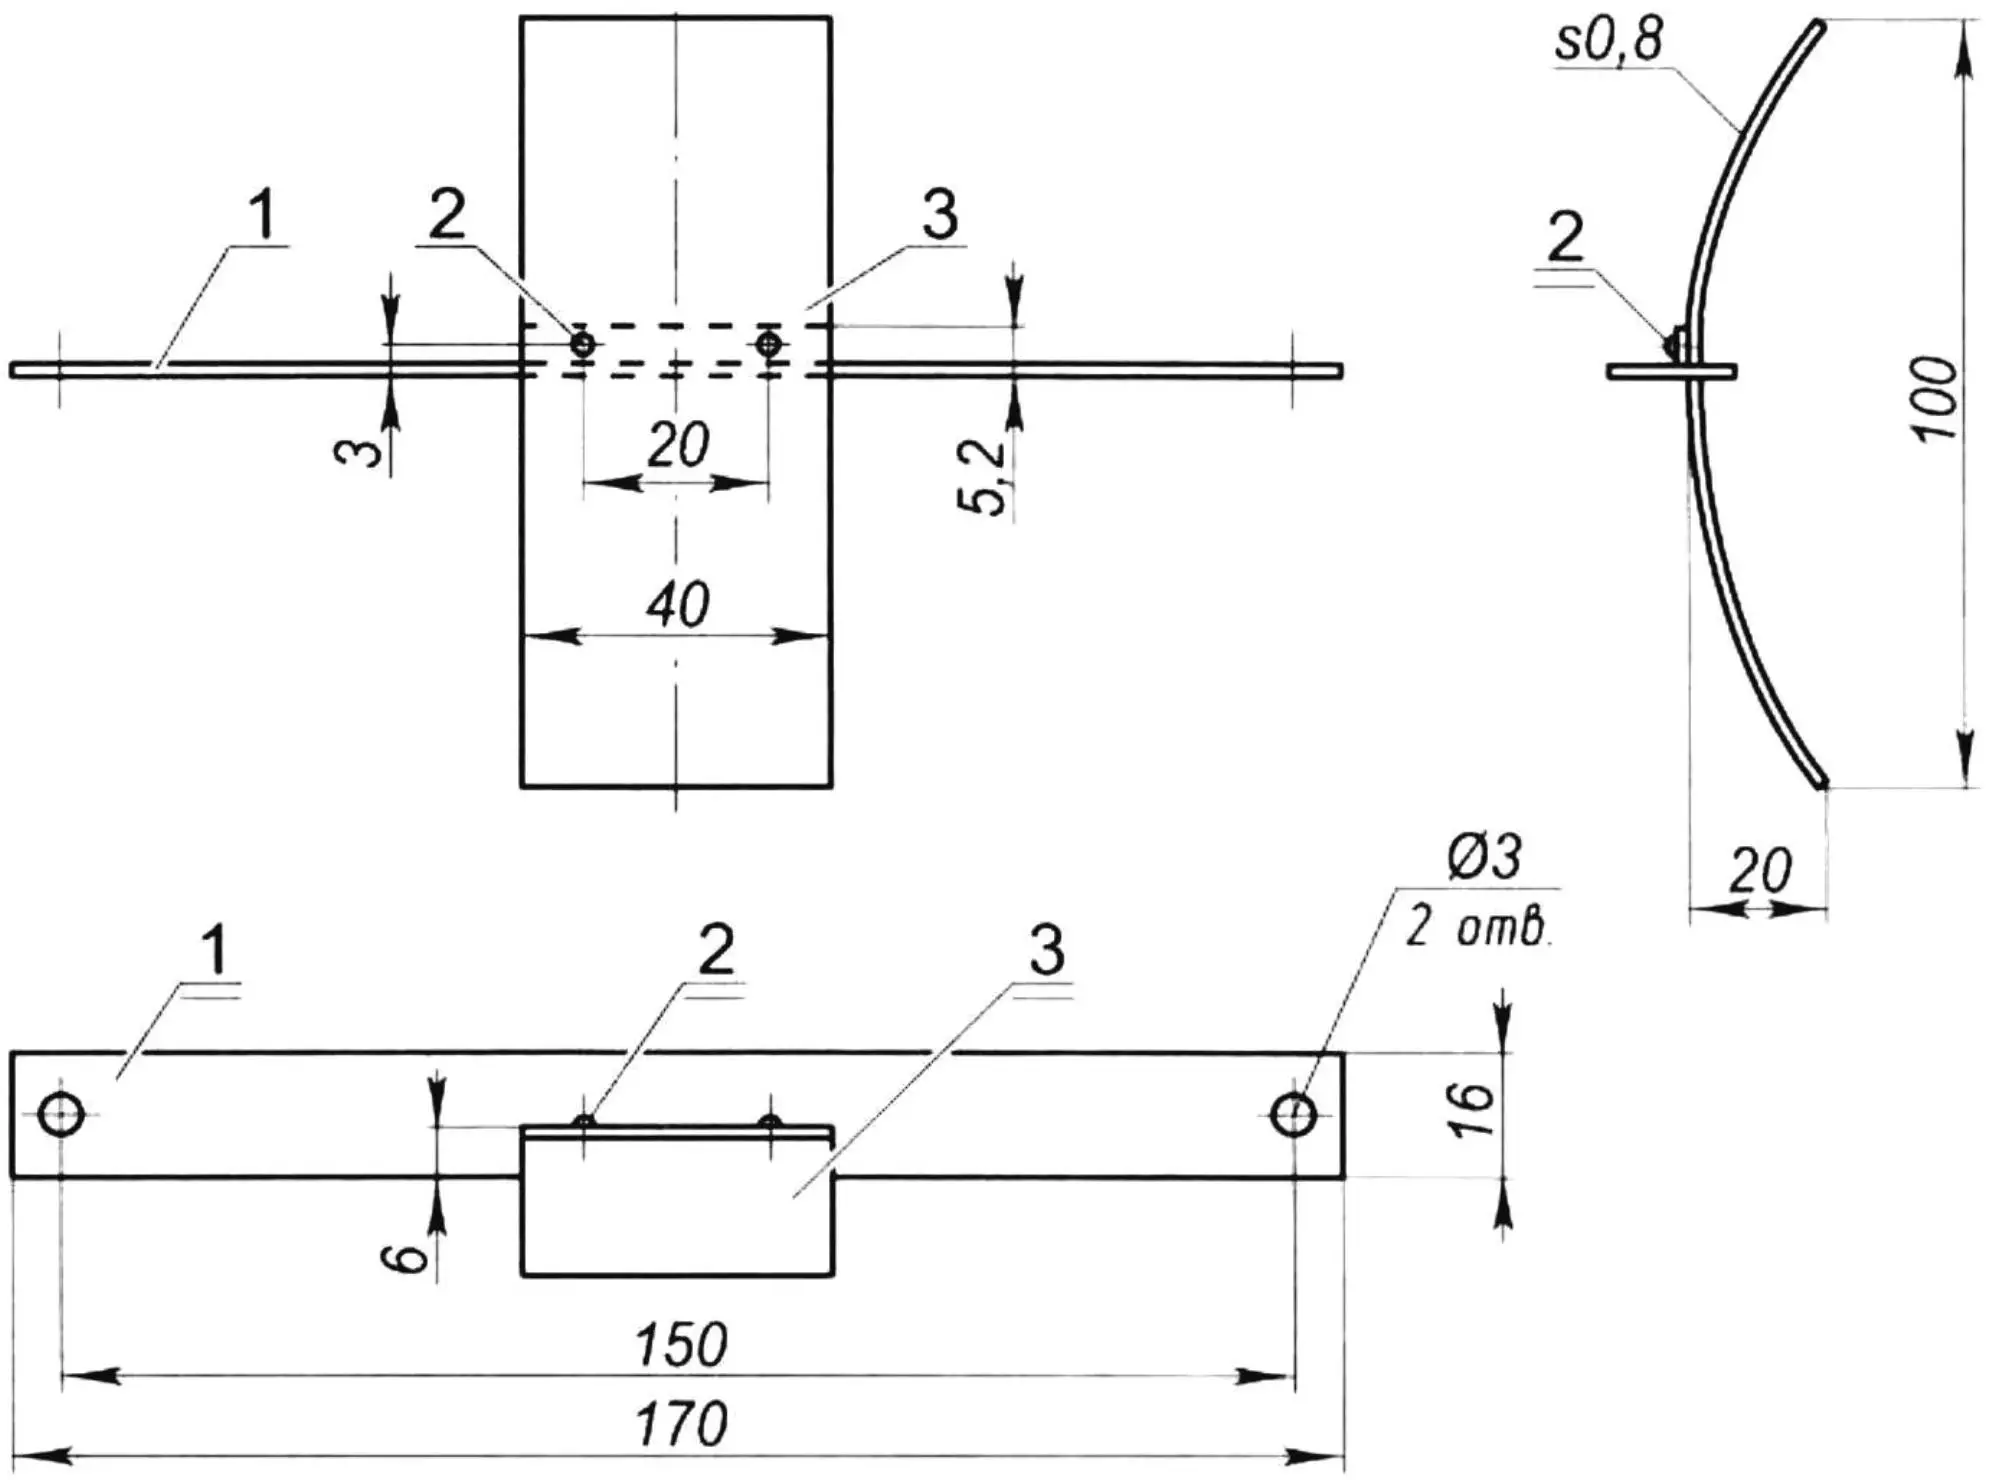
1 — bracket (sheet metal s0.8); 2 — rivet (Ø2×4, 2 pcs.); 3 — visor (sheet metal s0.8)
The amount of coolant should be such that the cutting disc is immersed in it by 8–10 mm. Next, 30–40 g of abrasive powder is poured into the tray near the cutting disc on the trough side. The powder can be obtained from a worn silicon carbide grinding wheel (green). After the workpiece is secured on the support, it is lowered onto the cutting disc, the KCP lid is closed, and the motor is switched on. After 1–2 minutes a characteristic “rustling” should appear, meaning that abrasive is reaching the cutting disc and the stone-cutting process has begun. In the first minutes, when resistance to tool rotation is low, a voltage of about 6–8 V is set on the power supply with the switch. This makes it possible to reduce motor speed and reduce abrasive throw-off from the cutting disc. As the cut deepens, the voltage supplied to the motor should be gradually increased.
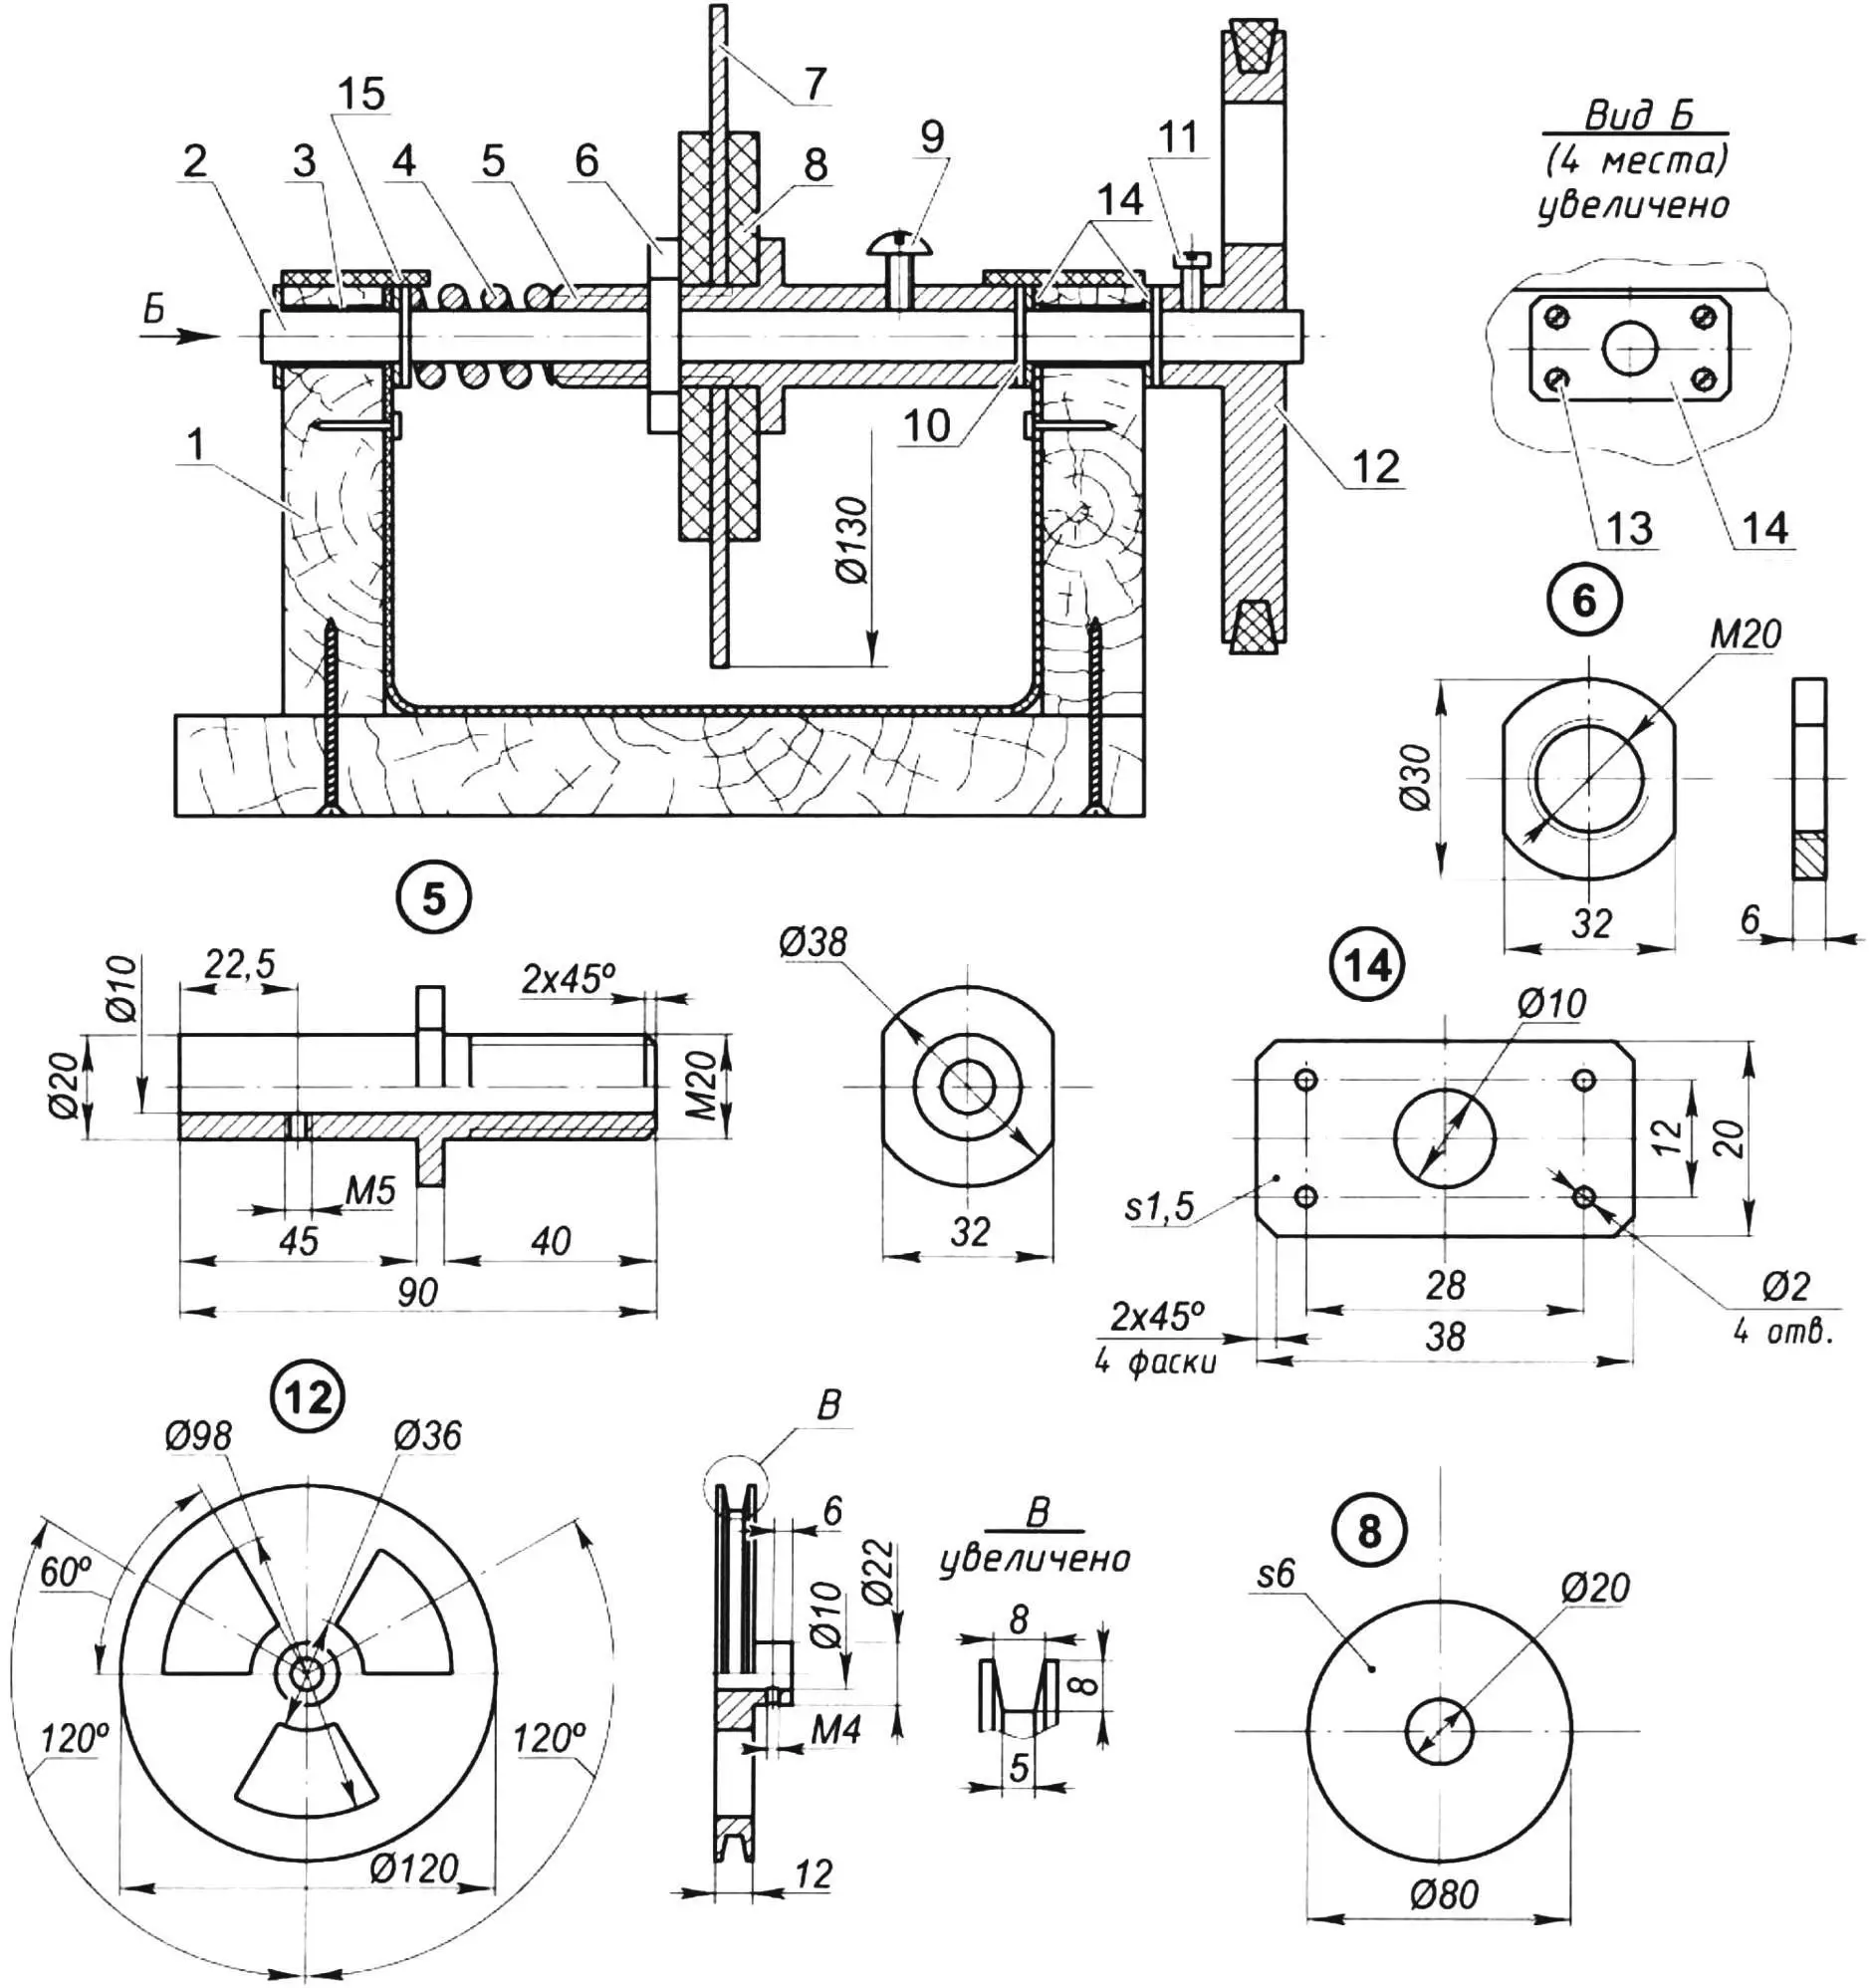
1 — base; 2 — shaft (steel 45, round bar 10, L195); 3 — heat-resistant grease; 4 — compression spring (OVS wire s0.8); 5 — bushing (duralumin, round bar 38); 6 — cutting disc fastening (M20 nut); 7 — cutting disc (sheet metal s0.8); 8 — pressure washer (textolite s6); 9 — bushing lock (M5 screw); 10 — washer (steel, sheet s1.5, 3 pcs.); 11 — pulley lock (M4 screw); 12 — pulley (duralumin, round bar 120 or sheet s12); 13 — screw (2×10, 16 pcs.); 14 — bearing plate (steel, sheet s1.5, 4 pcs.); 15 — reflective strip
As can be seen from Figures 3 and 5, the base supports have different heights: the front one (at the trough) is 20 mm, the rear one is 50 mm. This is done so that abrasive powder thrown toward the rear wall “flows” back to the cutting disc. If necessary, the KCP can be rigidly clamped to a workbench — for this reason the base bottom is made 12 mm wider than the side walls.
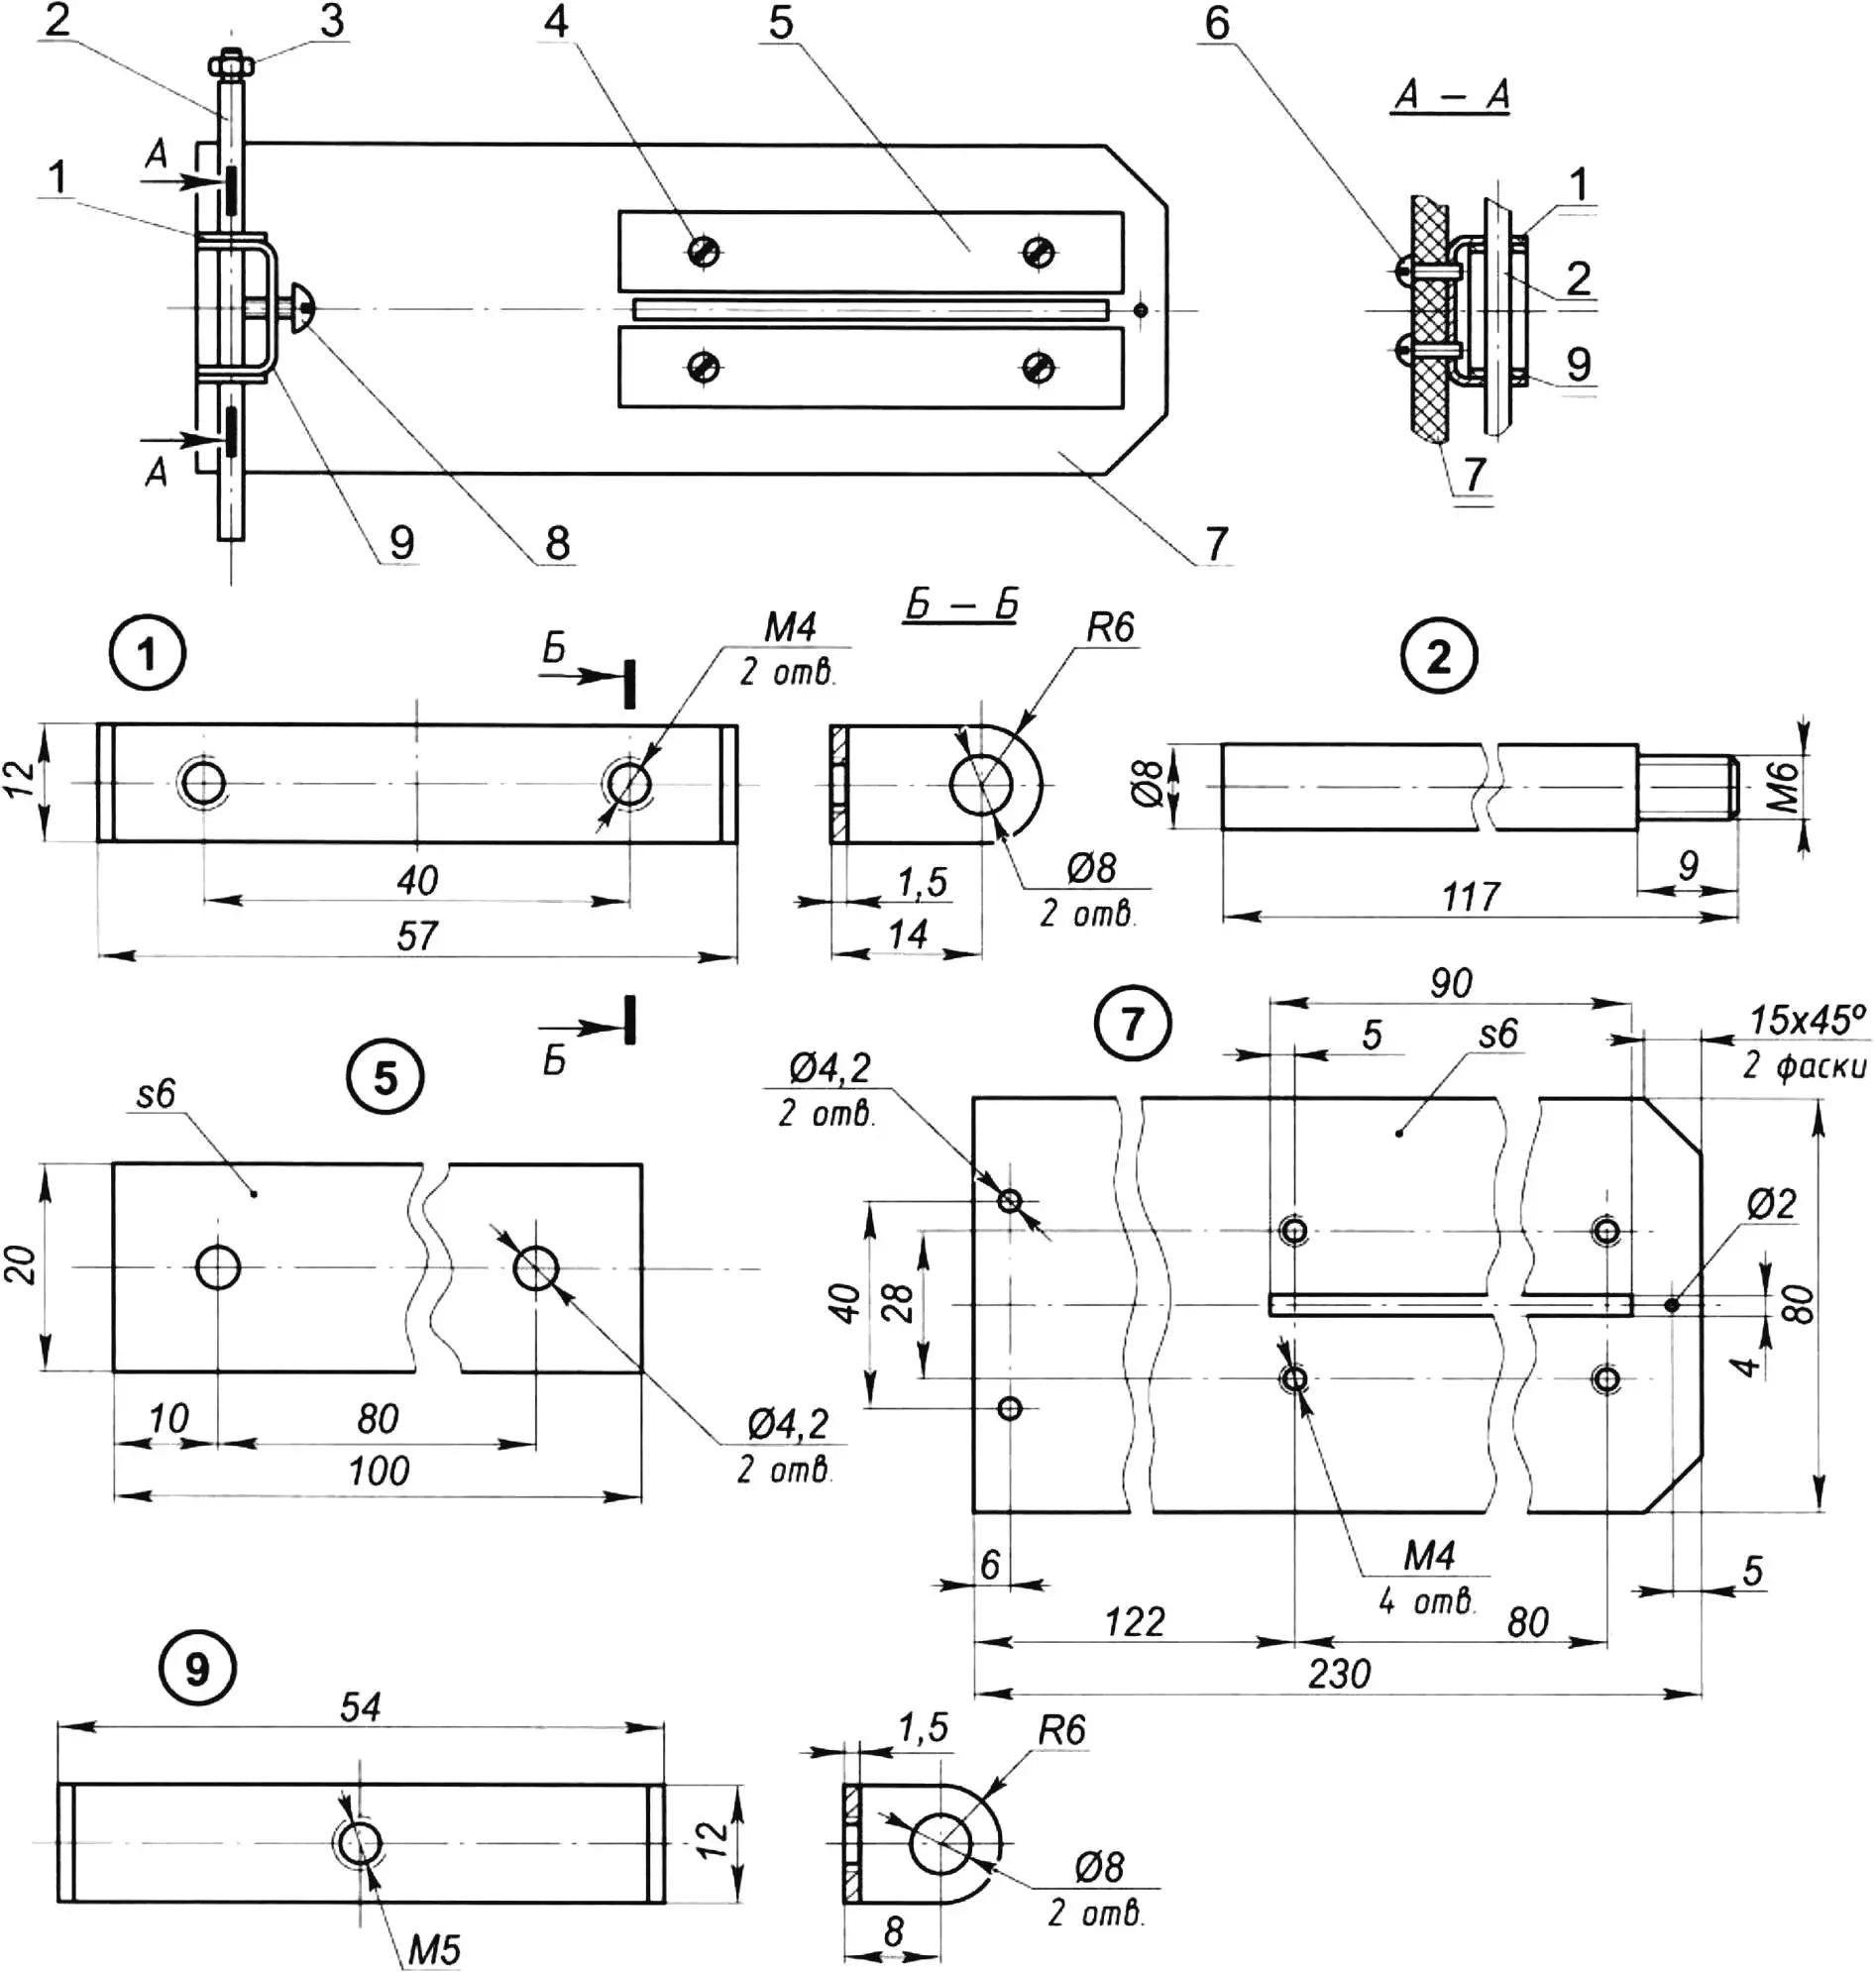
1 — clamp (steel, bar 1.5×12); 2 — axle (steel, rod Ø8); 3 — M6 nut; 4 — bar fastening (M4x40 screw, 4 pcs.); 5 — bar (textolite, getinaks, s6, 2 pcs.); 6 — clamp fastening (M4x10 screw, 2 pcs.); 7 — plate (textolite, getinaks s6); 8 — lock (M5 screw); 9 — inner clamp (steel, bar 1.5×12)
After finishing work, the coolant is drained through the trough, the abrasive is removed from the tray (for later use), the tray is rinsed with warm water and dried.
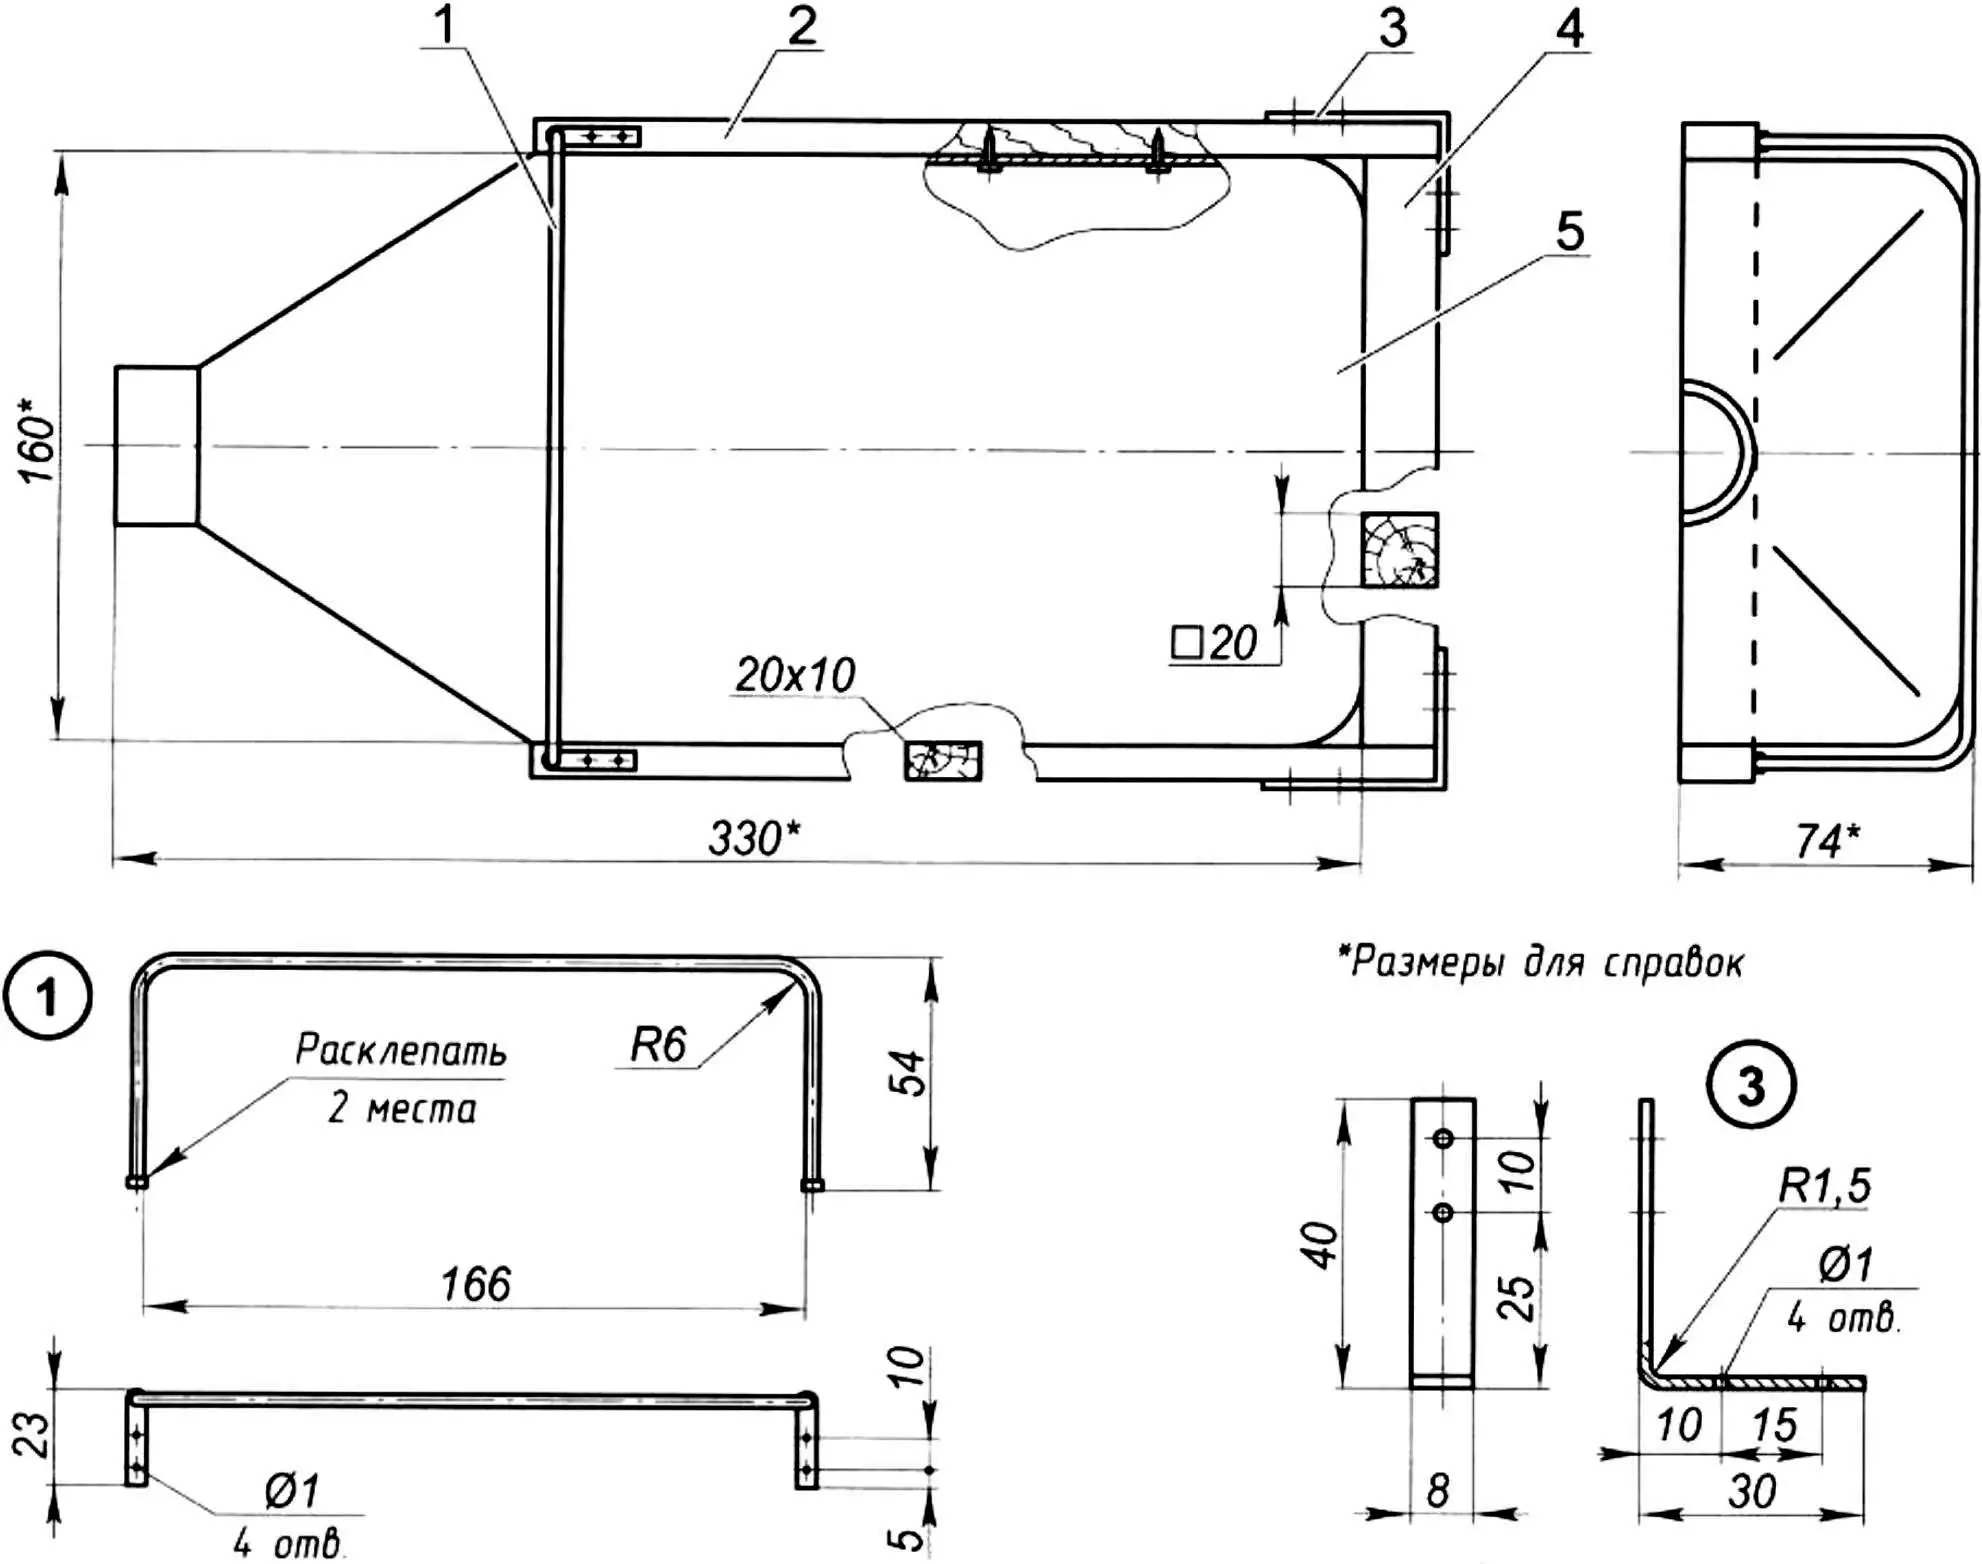
1 — clamp (wire Ø3); 2—side member (birch, bar 10×20, L210, 2 pcs.); 3 — angle (sheet metal 0.8, 2 pcs.); 4 — crosspiece (birch, bar 20×20, L160); 5 — housing (half of a plastic 5 L bottle)
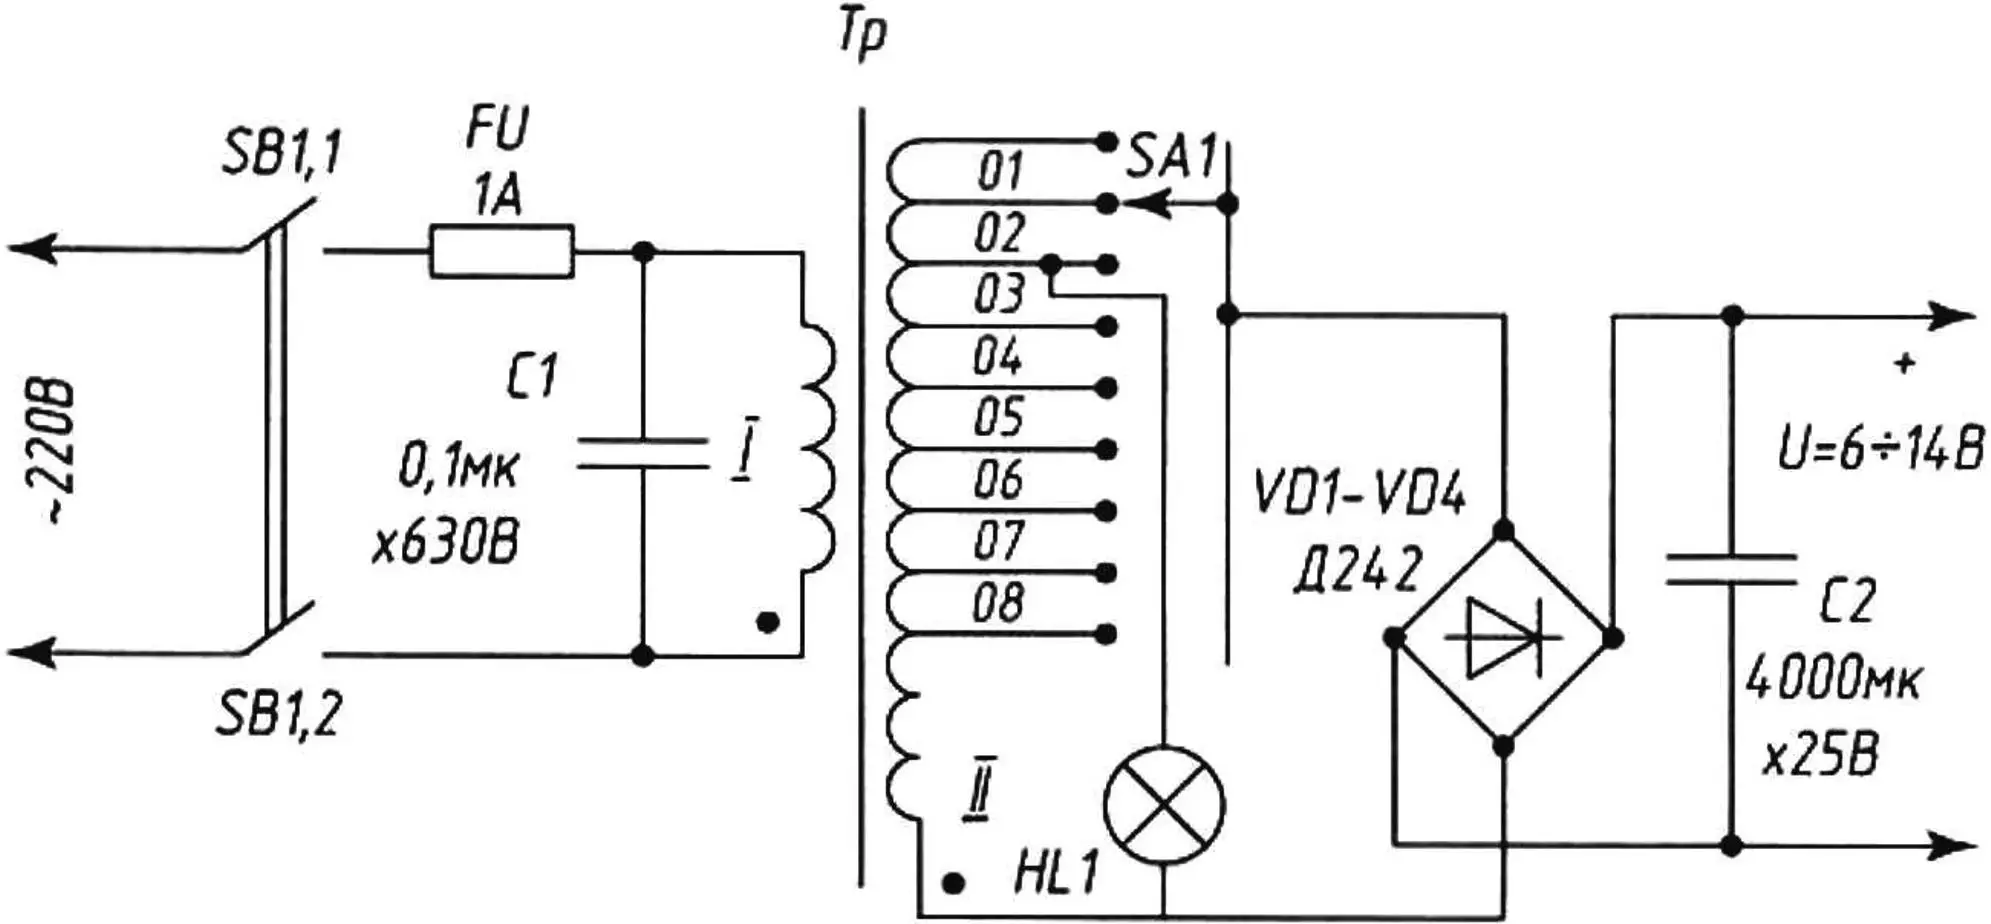
The power supply unit (the schematic diagram is shown in Fig. 2) has a standard design. A modified TS-180 (from an old vacuum-tube TV) is used as the transformer. The secondary windings on its coils are replaced with new ones wound with insulated copper wire of 2.5 mm2 cross-section (see the table).
Number of turns and voltages in the secondary windings
| Winding II | Winding III | |||||||
|---|---|---|---|---|---|---|---|---|
| Numbers Start of leads — 01 | 01-02 | 02-03 | 03-04 | 04-05 | 05-06 | 06-07 | 07-08 | 08-end |
| Number ×20 turns | 3.5 | 3.5 | 3.5 | 3.5 | 3.5 | 3.5 | 3.5 | 3.5 |
| Voltage, V | 6 | 1 | 1 | 1 | 1 | 1 | 1 | 1 |
Switch SA1 is of the PGK-1-11 type; signal lamp HL1 is 12 V, 90 mA; capacitor C1 is of the BMT-2 type, C2 is K50-6; the power switch is of the TP1-2 type. Diodes DV1–VD4 (D242) are mounted on an aluminum plate 5 mm thick measuring 80×100 mm and insulated from it with mica washers. Wiring is done with BPVL wire of 1.5 mm2 cross-section. The power supply is covered with a housing (of roofing iron) measuring 190x140x120 mm.
If making the power supply unit is difficult, the KCP can be powered from any 12 V DC source, for example a car battery or a charger for it.
KCP technical data
Saw disc speed, rpm … 600 – 800
Cutting rate, mm/min up to … 1
Maximum stone thickness, mm … 25
Supply voltage (mains), V … 220
Power consumption, W … 120
“Modelist-Konstruktor” No. 3’2010, L. STEPANOV
Recommend to read
 ON ONE BOARD WITH A SAIL
Of course, sailing the Board someone able to buy in the store. However, most can't afford it. Such will want to do it yourself. Especially since there is no design supercomplex forms. To... MISSILE “STORM”
In accordance with the existing plan for the construction of the Soviet Navy in the late 1950-ies provided for the construction of a series of special vehicles, air defense PR 1126 ships...
